Enzyme preparations are produced via mature submerged liquid fermentation under fully sealed and sterile control. The entire process consists of five standardized stages: strain cultivation, submerged fermentation, separation and purification, formulation processing, and finished product inspection, which guarantee stable enzyme activity and consistent performance across batches.
The first stage involves strain activation and stepwise scale-up. Drawing on our proprietary strain library, we screen and genetically modify strains to develop high-yield engineered strains tailored to market demands. Cryopreserved original strains are revived and activated in sterile test tubes, followed by primary cultivation in shake flasks before being transferred to multi-stage seed tanks for gradual amplification. Technicians monitor temperature, dissolved oxygen and pH values in real time while maintaining strict sterile conditions to prepare vigorous, contamination-free seed liquid for subsequent fermentation.
Submerged fermentation is the core stage where enzymes are synthesized. Qualified seed liquid is transferred to large automated fermenters filled with compound media formulated with carbon and nitrogen sources. Equipped with intelligent sensors that monitor fermentation conditions round the clock, the system adopts fed-batch fermentation to supply nutrients continuously, enabling microbes to metabolize steadily and secrete target enzymes. After dozens of hours of constant-temperature fermentation, crude enzyme broth is obtained. Compared with chemical synthesis, this bio-fermentation process generates far fewer pollutants and aligns with green and low-carbon manufacturing standards.
Post-fermentation, the broth proceeds to separation and purification. Mycelia and solid residues are removed via plate-and-frame filtration and membrane filtration. Ultrafiltration concentration and chromatographic purification are then applied to enrich active enzymes and eliminate miscellaneous proteins and soluble impurities, significantly improving enzyme purity while minimizing activity loss. All operations are conducted in closed systems to prevent secondary contamination.
Purified enzyme liquid moves on to customized formulation. Products are tailored for diverse industries: liquid enzymes are blended with dedicated protectants to make concentrated formulations; solid enzymes are spray-dried into homogeneous powder, compounded with carriers and stabilizers to enhance heat resistance and storage stability, suiting processing scenarios in food, feed, textile and other sectors.
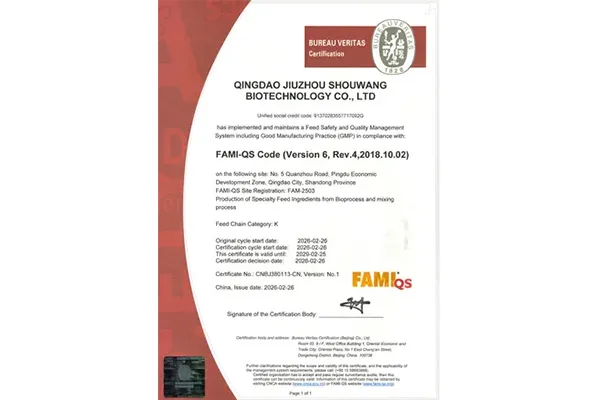
All finished products undergo comprehensive testing in professional laboratories to verify enzyme activity, microbial limits, heavy metal content and impurity levels. Only qualified products are aseptically packaged and stored for delivery. The full closed-loop fermentation chain is independently controlled from strain development to finished goods delivery, enabling consistent production of high-quality, stable industrial enzymes. Our biocatalytic solutions support clean production across all industries.
 English